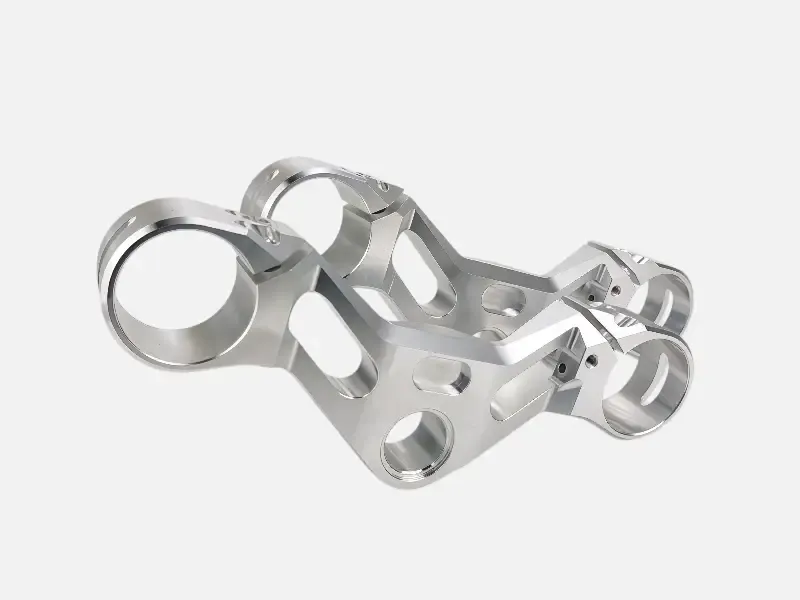
Custom precision machining parts with a tolerance up to ±0.005 mm, from single prototypes to production runs.
Stainless steel is ideally used in difficult working conditions, such as exposure to saltwater, aggressive chemicals, humidity, food, or high temperatures. It resists corrosion and maintains its mechanical properties
Stainless steel is an iron-based alloy containing a minimum of 10.5% chromium. This chromium reacts with exposed surfaces, forming a protective oxide layer that prevents corrosion. 304 grade handles fresh water, humidity, and mild chemicals well. Marine 316 grade has 2% molybdenum content, closing the chloride and salt spray resistance gap.
Austenitic grades (304, 316) keep toughness at cryogenic temperatures as low as -196°C, being standard for LNG handling, cryogenic equipment, and medical gases equipment.
A combination of corrosion resistance and high mechanical properties results in higher service life than carbon steel in any moist, chemical, or cyclical temperature environment.
Stainless steel is 2-3 times stronger than most aluminum alloys and has good mechanical properties. Martensitic grades such as 17-4 PH can reach tensile strength of 1,300+ MPa with precipitation hardening.
There are over 150 variants of stainless steel, and they can be subdivided into different categories, including austenitic, ferritic, martensitic, duplex, or precipitation hardening varieties. 304 and 316 are the most common stainless steel grades and cover the majority of industrial, food contact, and architectural applications.
| Property | 304 | 316 |
|---|---|---|
| Main alloying elements | 18% Cr, 8% Ni | 16% Cr, 10% Ni, 2% Mo |
| Tensile strength | ~515 MPa | ~515–580 MPa |
| Yield strength | ~205 MPa | ~205–240 MPa |
| Density | 7.93 g/cm³ | 7.99 g/cm³ |
| Machinability | Good | Fair |
| Corrosion resistance | Humidity, fresh water, mild chemicals | Chlorides, salt spray, chemical environments |
| Weldability | Excellent | Excellent |
| Relative cost | Lower | Higher (~15–25% on material) |
| Best for | Food equipment, industrial housings, architectural | Marine, chemical processing, medical, pharmaceutical |
Free-machining austenitic grade with added sulfur for improved chip-breaking performance. Best machinability among all austenitic stainless steels. Preferred for machining high-volume turned parts with threads and complex geometry.
Free-machining martensitic grade, heat-treatable. Good machinability and some ability to increase strength by heat treatment. Used in shafts, gears, and valves requiring both machinability and moderate strength.
Precipitation-hardened grade capable of reaching tensile strength up to ~1,310 MPa. Good corrosion resistance. Standard grade in aerospace, medical, and high-load structural applications.
Martensitic grades, capable of reaching high hardness in heat treatment. 440C grade hardness can be increased up to 58–60 HRC — suitable for valves, bearings, cutlery, and surgical instruments.
Note: Custom grades are available upon request. Provide the material spec, and we’ll check its machinability and processing capabilities.
Stainless steel is naturally corrosion-resistant in many environments, but the right surface finish matters for cleanability, appearance, corrosion resistance, and application requirements.
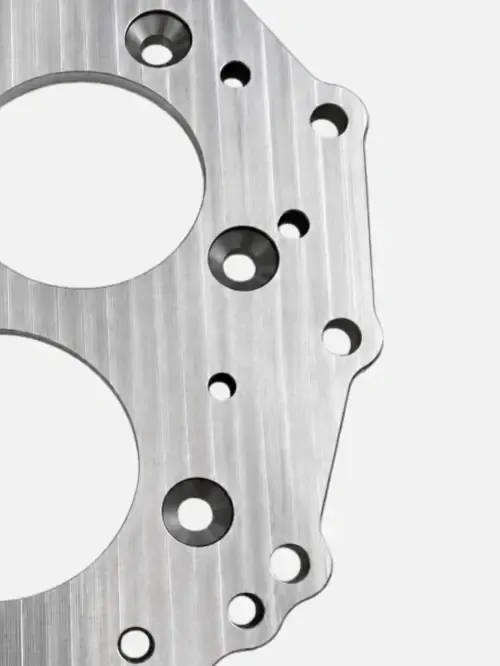
Visible machining marks with a typical Ra 3.2–6.3 μm surface roughness, ideal for functional parts
Usually using nitric or citric acid, which removes free iron from the surface of machined parts
Mechanical polishing to Ra 0.2-0.8 µm for satin/mirror finish, or electropolishing for smoother finish
Note: Other stainless steel parts finishes, including brushing, bead blasting, and plating, are also available upon request.
See some of the CNC machining stainless steel parts we’ve made, highlighting different materials, machining methods, and production challenges.
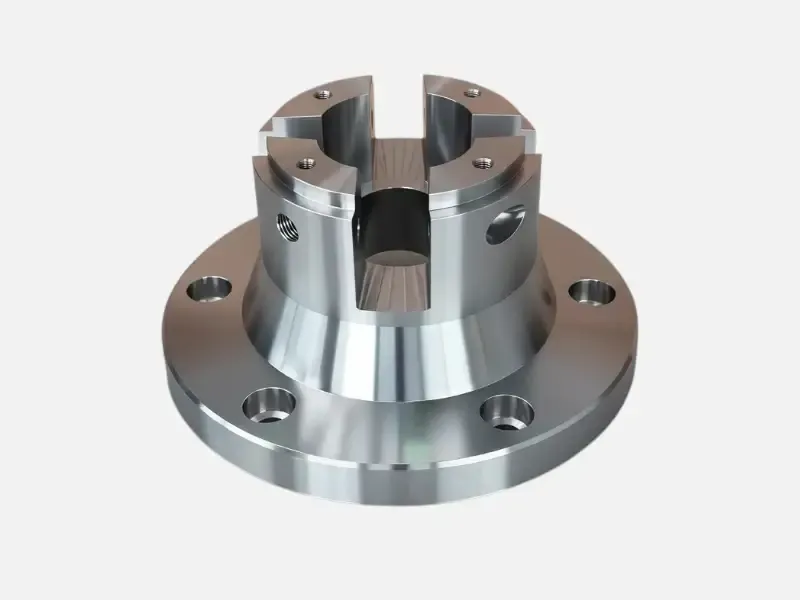
Requirements were coaxiality of bore and outer diameter, perpendicularity of the flange face, and accuracy of the bolt hole pattern. In this case, clamping distortions turn into coaxiality and perpendicularity errors. We controlled the clamping force and machined the bore and outer diameter in one setup to eliminate coaxiality error caused by rechucking. The bolt holes were machined in a single setup from the bored center.
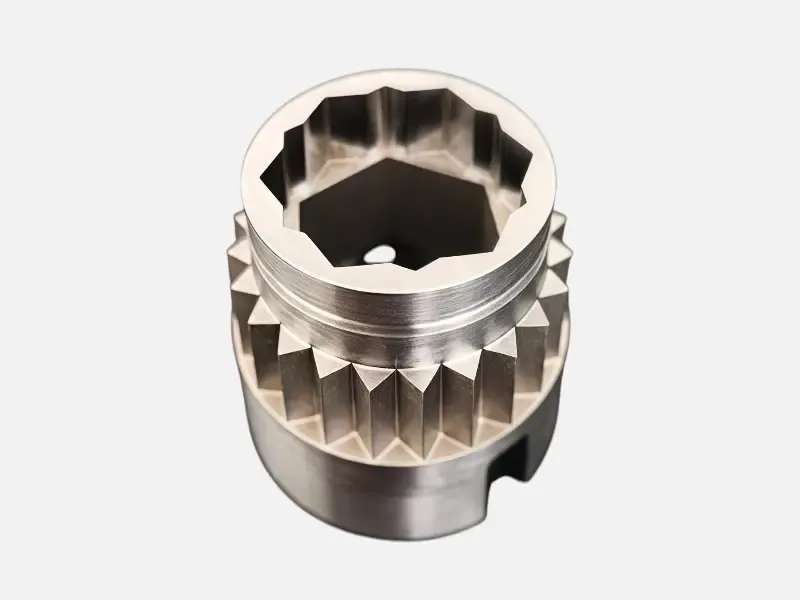
The correct type of 303 stainless steel for this part. The increased content of sulfur helps in chip breaking on small diameters, making it possible to hold the geometry of threads and tooth profiles on the part with very shallow stock removal per pass. The biggest problem was the coaxiality of the inner and outer cylindrical surfaces along the whole length of 47 mm. The part was mill-turned between centers with a finishing cut that brought the inner and outer surfaces to coaxiality within tolerance.
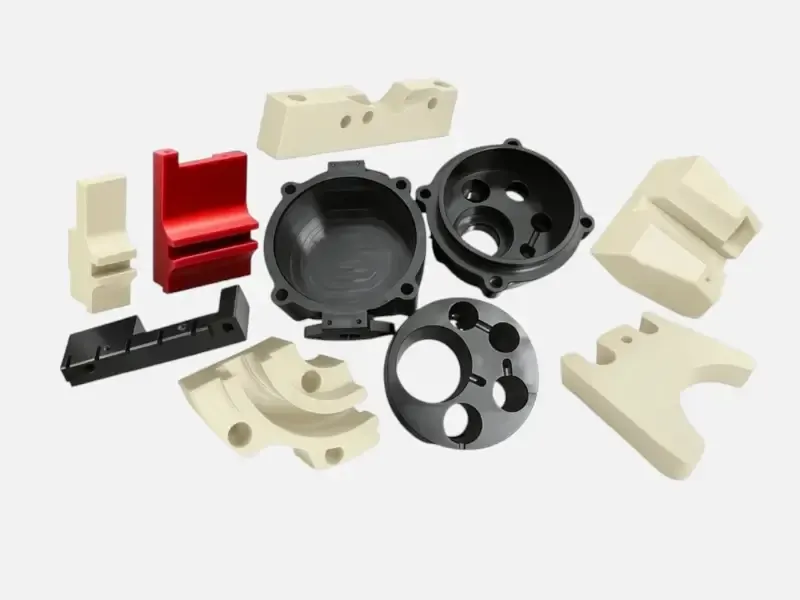
There were two major challenges for the part. One is workholding of this big, multi-faced part without distortion. Another is control of wall deformation while removing material to form a relatively thin-walled structure. We developed a special fixture that loads the part from structural elements rather than from thin walls and planned roughing and semi-finishing cuts sequentially to release stresses of material gradually before final finishing cuts. The resulting part meets the vacuum integrity and dimensional tolerance requirements
In addition to stainless steel CNC machining services, we also provide machining services for steel, aluminum, and other engineering metals and plastic materials.
304 is the standard type – good corrosion resistance and machinability, cheaper. 316 includes additional molybdenum that increases significantly the resistance to pitting and salt spray corrosion. Use 304 for indoor, general industrial, and food contact applications. Order 316 for marine and chemical processing applications or whenever the environment regularly contains chloride or salt.
Yes, mostly due to work hardening. Grades 304 and 316 harden rapidly if a tool rubs rather than cuts; this happens mostly with dull tooling or low feed rates. Cycle time is usually 50-100% longer than for comparable carbon steels. The exception is 303, increased content of sulfur makes it similar to carbon steel and is the correct type when machinability is the priority.
No. 304 and 316 in as-machined condition provide sufficient rust resistance in most indoor and non-chloride environments. If you require salt spray, high humidity, or hygiene-critical conditions, passivation is recommended – it increases significantly the strength of the oxide film significantly and is a standard practice for medical and food contact stainless products. Polishing is used for cleanliness and aesthetic purposes, not for corrosion prevention.
The general dimensions comply with ISO 2768-m tolerances. Unless dimensions marked on drawings. Critical dimensions with high tolerance are held to ±0.005 mm. For small diameter turned parts, coaxiality and concentricity are held to 0.005-0.01 mm TIR.
Yes. 17-4 PH is machined best in the annealed state (Condition A). The general sequence is rough machining, precipitation hardening to the required hardness (H900 through H1150), then finish machining or grinding. Hardness after aging is about 28-44 HRC depending on aging temperature. We plan the machining sequence with account of dimensional change during precipitation hardening.
Passivation is a chemical process – usually nitric or citric acid – that removes free iron from the surface of machined parts and increases the passive film of chromium oxide. Passivation is required for food contact, medical and pharmaceutical parts, for chloride or elevated humidity environments, and when machining contamination may affect the passive layer. Does not change dimensions and appearance and is an economic option for the parts.
Add: Building F, No.2 Nanling Road, Xin'er Community, Xinqiao Subdistrict, Bao'an District, Shenzhen, Guangdong Province, P.R.China
Email: 1281883259@qq.com
Phone: +86 18948799832